.png)
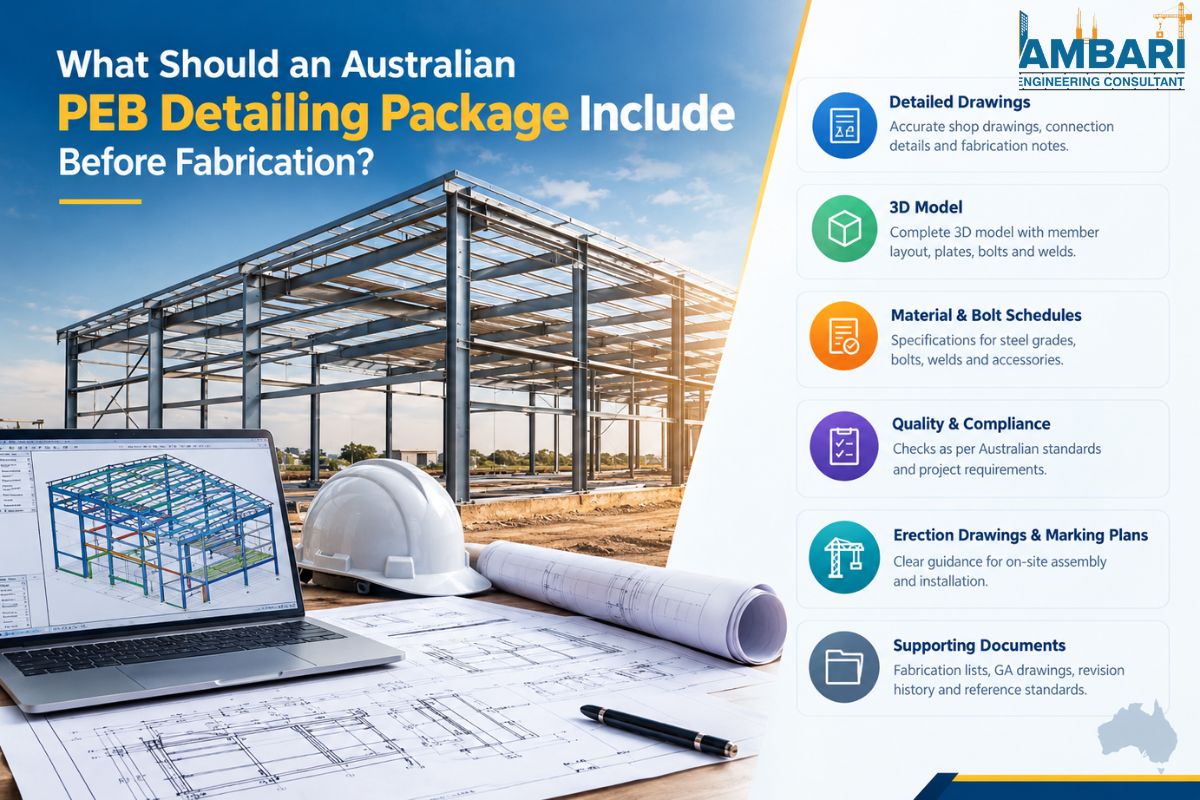
PEB, which is typically referred to as pre-engineered buildings, is an efficient building type. They provide large clear spans at reasonable cost with tapered or built-up sections, standardised connections, and light cladding. Precision is the key to that efficiency. If one part of a base plate hole position is mis-set or if one bolt is not used, it can halt a whole erection crew for a day.
In Australia, many projects are rushed from design to fabrication, often due to pressure from the builder, the developer, or the steel supplier. During that frenzy, sometimes packages are approved piecewise. The primary members are cut during the review of the connection detail while the fabricator is still working. This is where many difficulties start: A full package seals these holes while cutting is not performed.
It also safeguards the individuals concerned. The engineer receives a set of documents matching the design. The fabricator receives drawings that it can produce without interpretation. The erector receives a sequence that maintains the frame stability through the staged process. The client receives a building that is built to the approved design and standards.
A complete package consists of design basis, general arrangement drawings, member schedules, connection details, fabrication and erection drawings, cladding layouts, coating specifications, quality records, etc. These documents are one-way and iterative. If any of the earlier documents, like a design basis, is incorrect, then the same error will be propagated through all of the later drawings. So, it is important to look at the package as a whole, not a single sheet.
Pre-engineered packages typically come in the form of layers. The main frame design is made by the manufacturer. The design is checked by an engineer in the local area, who is knowledgeable in loading and structural codes and standards applicable to Australia. The detailer then creates shop and erection drawings of the approved design. All the layers should be based on the same grid lines, member marks, and revision numbers.
The design basis is the whole package basis. It includes the loads, codes, and assumptions for sizing the frame. If it is not there, no one can ensure the connections of the building are sufficient for the building. Wind actions are usually evaluated by AS/NZS 1170.2 in Australia and seismic actions (if applicable) by AS 1170.4. The parameters to be used should be clearly dictated by the design basis.
A proper design basis normally includes:
Therefore, if any are absent, request them before fabrication. For example, if a crane load is not found, the column sizes and base plate requirements could completely change.
GA drawings (known as general arrangement drawings) depict the entire structure of the building. These include plan views, elevations, sections, grid lines, bay spacing, eave and ridge heights, and roof slope. They also indicate the locations of doors, windows, mezzanines, and canopies. All other drawings in the package are based on these drawings, so their grid labels and dimensions should be identical.
The good GA set usually exhibits:
Moreover, all dependent drawings should be changed when a GA drawing is changed. A lot of detail mistakes happen as a result of an updated GA that isn't reflected in the connection details.
Every primary member, secondary member, and bracing member is identified by its section size, steel grade, length, and number in member schedules. The information becomes plate, bolt, and accessory quantities in the bill of materials. They can be used together to enable the fabricator to order the material, to plan cutting, and to ensure there is no missing material prior to work commencement. Additionally, they serve as a reference to verify the delivery of steel when it arrives.
Each member should have a clear mark, which is the same as the drawings. Common marks include rafter, column, purlin, girt, eave strut, and bracing. If the shop is cutting dozens of identical pieces, there is no need to worry about confusion due to inconsistent naming. It becomes highly likely that a mistake could be made if a rafter is labelled R1 on one drawing and RF1 on another.
A good member schedule and bill of materials should contain:
The quantities in the bill of materials should be the same as on the GA drawings and connection details. A mismatch occurs when only one document is revised. This can be caught by a quick visual cross-check between the member schedule and the drawings before cutting begins.
Each piece of steel should be described by a grade which corresponds to the appropriate Australian or New Zealand standard. The following table lists some typical items to check out before the order.
| Material Item | What to Confirm | Why It Matters |
|---|---|---|
| Structural plate | Grade and thickness as per design, to AS/NZS 3678 | Weld quality and bearing capacity |
| Structural sections | Grade as per the AS/NZS 3679 series | Member strength and stiffness |
| High-strength bolts | Grade and fastener set per AS 1252 | Connection capacity and preload |
| Welding consumables | Matched to parent metal and welding procedure | Weld strength and toughness |
| Galvanised items | Coating process per AS/NZS 4680 | Long-term corrosion protection |
Primary members and critical plates should be requested for mill test certificates. When a question comes up at some later point, the team is able to trace back to the corresponding heat number in the piece.
This is especially important when delivering mixed consignments on larger projects, as identification may be challenging.
Connection details establish the seamless integration of members and the flow of loading in the frame. They include base plates, anchor bolts, end plates, cleats, splices, and haunches. All connections require dimensions, bolt layout, weld sizes, and tolerances. One of the most frequent reasons for delay on a PEB project is the lack of clarity or detail in the connection.
Connections are where design intent meets the real steel. A beam can be designed to carry a given moment, but the ability to carry that moment is dependent on the thickness of the end plate, the bolt pattern, and the weld detail. If left to the fabricator, all of these could be different from the design.
All base plates and anchor bolts need to be coordinated with the civil foundation drawings. The size, thickness, and location of the holes must match, along with the diameter of the anchor bolts, the depth of penetration into the slab, and the height above the slab to which the plate is raised. A few millimetres out from all of the columns can make it so that they will not sit properly on the base plate. That is why it is important to clearly specify set-out and template tolerances in the package.
Some important things to verify are:
Correct any discrepancies between the foundation drawings and anchor bolt layout before fabricating. It is costly and time-consuming to correct anchor bolts after they have been cast in concrete.
Detail all rigid frame haunches, eave connections, ridge splices, and column-to-rafter connections. The drawing should include bolt pattern, end plate thickness, stiffener locations, and weld details. Splice sites need to be planned considering the transport distance and the crane capacity. Even a good splice that is installed in an awkward position can cause problems when erecting.
Fabrication drawings are also known as shop drawings and depict each piece as it will be cut, drilled, and welded. The ones that are included are piece marks, dimensions, hole locations, weld symbols, surface finish, and shop notes. The approved design is then sent to the workshop and is used to make the drawings by a professional PEB fabrication drawing services in Australia, so that the engineer's intent is not misinterpreted by the workshop. Fabrication drawings with clarity minimize questions on the shop floor and ensure an accurate fabricated steel component.
Fabrication drawings are also used to communicate the design to the manufacturing processes. They explain what each piece is going to be; the design explains what each piece should do. The two, when aligned, are able to work swiftly and confidently in the shop.
The pieces should be marked individually with a piece mark. The overall dimensions, hole diameters, edge distances, and cut lengths are as shown in the drawing. The piece marks should be next to the cutting list and bill of material. If this is not done, the shop can make the correct cross-sectional steel but the wrong length or make parts that will not assemble.
A good fabrication drawing typically contains:
Moreover, this is the more detailed level that Strong Steel fabrication drawings services in Australia specialize in, as this is where small mistakes can cost dearly. A drawing which is correct to the millimetre saves hours of rework later.
The fabricator is to follow the standard for welding symbols AS 1101.3 to ensure that they interpret the symbol as the detailer intended to communicate. Bolting specifications should be clearly identified. The drawing should indicate if the bolt is snug tight or pretensioned, as this will influence the inspection and installation procedure depending on the bolt connection category as per AS 4100. Hole symbols should identify drilled holes, punched holes, and sub-punched and reamed holes.
If you must have the bolt holes pass through two pieces, then the tolerance must be specified on the drawing. The holes that are not aligned are a common cause of site delays, as the erector has to enlarge holes or flame cut members, neither of which should occur in the field.
Erection drawings indicate the way the frame should be joined on location. These consist of the erection sequence, crane positions, lifting points, temporary bracing, and the sequence of bolt tightening. A reliable Steel structure erection drawing service in Australia creates these drawings before any work begins in the shop to ensure the fabricator has the pieces marked, the trucks are loaded in the right sequence, and the site is set up for stability.
Many people believe that erection drawings are only used at site. In practice, they affect the manufacture. The pieces to be packed first, the placement of lifting points, and the position of splices are all determined by the erection plan. When the erection sequence is determined after the pieces have been fabricated, the shop might have to re-mark and re-sequence late.
The PEB frame is not stable until it has a sufficient number of members and bracing. The sequence of erection should indicate the construction of the frame piecemeal, and where temporary bracing is required. Sometimes the temporary bracing is omitted at this stage, and the drawing should indicate precisely when and under what circumstances each brace can be removed.
The following should be included on erection drawings:
Should include lifting points, rigging arrangement, and approximate weight of each piece. This information is used by the crane's operator and rigger to plan safe lifts. Ground bearing conditions, access routes, and crane radius should also be discussed early as they will influence the construction of the frame. A seemingly easy-to-construct frame may turn out to be tricky if the crane does not have the necessary positions to access the structure.
It is common for cladding layouts, openings and accessories to be considered as secondary elements, but there are several ways in which they impact the primary frame. The spacing of purlins and girts will be determined by the cladding system. Trimmers and headers are needed for door and window openings. Mezzanines require beams, joists, and deck elements to tie to the main structure. These items should be detailed as part of the package, not added later.
The layout of the cladding is presented, indicating the position of the roof and wall sheets, sheet lengths, laps, fixing information, and flashing information. Spacing for purlins and girts must conform to the requirements of the cladding manufacturer. Inaccurate spacing can result in non-support of sheets and cause deflection, leakages, or fixing failures.
Cladding details usually include:
Openings must be framed, and headers must be provided, along with trimmers. The package should contain information on their locations and link to the main frame. The detailing of mezzanines requires careful detail since they are under live loads and connected with the main structure. The connections of the mezzanine beam, the support for the floor deck, and the fixings for the stairs or handrails should all be illustrated.
Corrosion protection must match the building’s environment. AS/NZS 2312.1 provides recommendations on the type of coating to be used, depending on the exposure at which it is used, such as coastal salt, inland, industrial chemicals, etc.
The following table includes examples of typical exposure conditions as well as the details to confirm.
| Environment | Typical Concern | Detail to Confirm |
|---|---|---|
| Inland and dry | Low corrosion rate | Standard primer and topcoat system |
| Coastal or marine | High chloride exposure | Hot-dip galvanising or high-build coating |
| Industrial | Chemical fumes | Chemically resistant coating system |
| Wet or washdown areas | Standing moisture | Drainage details and sealed connections |
Surface preparation, dry film thickness and post erection touch up are also part of the coating specification. To prevent galvanic corrosion, the coating system should be compatible with bolts, washers and nuts. The points where galvanised and painted members connect to each other should indicate how they are protected at the connection.
The steel frame is not the only factor to consider. The steel is affected by the foundations, slab levels, drainage, electrical services, and cladding interfaces. These trades need to coordinate before fabrication. When the crew arrives at the job site, conflicts may not show up until a short coordination meeting is held.
It is good practice to have clash checking. It is a comparison of steel layout with other services and structures to catch conflicts at an early stage. Common clashes include:
All collisions should be documented, attributed to a specific person, and promptly resolved prior to drawings being issued for fabrication. This little process generates a lot of rework.
Some of the quality documents include inspection plans, welding procedures, welder qualifications, bolt tension records, dimensional checks, and mill test certificates. AS/NZS 5131 relates to the fabrication and erection of structural steel, and is frequently used concurrently with AS 4100.
The most useful application of these documents is to be able to agree before fabrication. Having the inspection hold points established ahead of time allows the fabricator to know when to request an inspection and the engineer to know what to look for.
A full quality set should comprise:
In Australia, before approving a PEB detailing package, check for revisions, grid lines, and member marks to avoid expensive fabrication and erection errors.
| Document | What to Verify |
|---|---|
| Design basis | Loads, codes, and parameters match the project brief |
| GA drawings | Grid, heights, and openings match the architectural layout |
| Member schedule | Quantities and marks match the GA and connection details |
| Connection details | Bolt patterns, plate sizes, and welds are complete |
| Foundation interface | Anchor bolts match the civil drawings |
| Fabrication drawings | Piece marks link to the cutting list and bill of materials |
| Erection drawings | Sequence, bracing, and lifting points are clearly shown |
| Coating specification | Suits the site environment and matches the drawings |
| Quality plan | Hold points and inspection requirements are agreed |
It is a good practice to get the detailer to make it very clear in writing which revisions have been made on each drawing. A large number of errors stem from a fabricator who was using an older revision, which had not been updated and was still in the shop. An erection drawing that is created with a steel structure erection drawing service in Australia should also be examined in conjunction with the site plan to ensure that crane access and laydown spaces are realistic.
Select a detailer who is familiar with the Australian standards, documentation, and communication. Ambari Consultant provides coordinated drawings from design to erection.
When shopping for providers, consider the following:
The lowest bid may mean that more is spent on the project. Look for providers that provide PEB fabrication drawings in Australia that have revisions, quality checks, and coordinated drawings. Check the compatibility of steel fabrication drawing services with design, erection plans, and quality documents in Australia.
The key to successful PEB detailing services in Australia is a well-prepared package. It condenses all the design information, drawings, schedules, connections, erection plan, and quality records into a single, unified set that the fabricator and erector can trust. Each document provides the same revision, and every detail is complete, so the steel is ready to assemble, the site operates more efficiently, and the final building is functional.
Even before you approve any package, do a thorough review of the package. One of the best ways to safeguard your schedule, your budget, and your reputation is to have that review.
The information usually provided includes design basis, general arrangement, member schedules, connections, fabrication drawings, erection drawings, and quality records.
They check sequence, bracing, lifting points, and the order of the bolts – pieces are marked, packed, and shipped in the correct order.
Check coating systems in design and prior to fabrication, as coating system selection can impact fixings, lead times, and shop scheduling.
Most rework is due to mismatched revisions, unclear connection details, and anchor bolt layouts that don't match the foundation drawings.